products
HomeProductsBJY PET Mold Core

BJY PET Mold Core

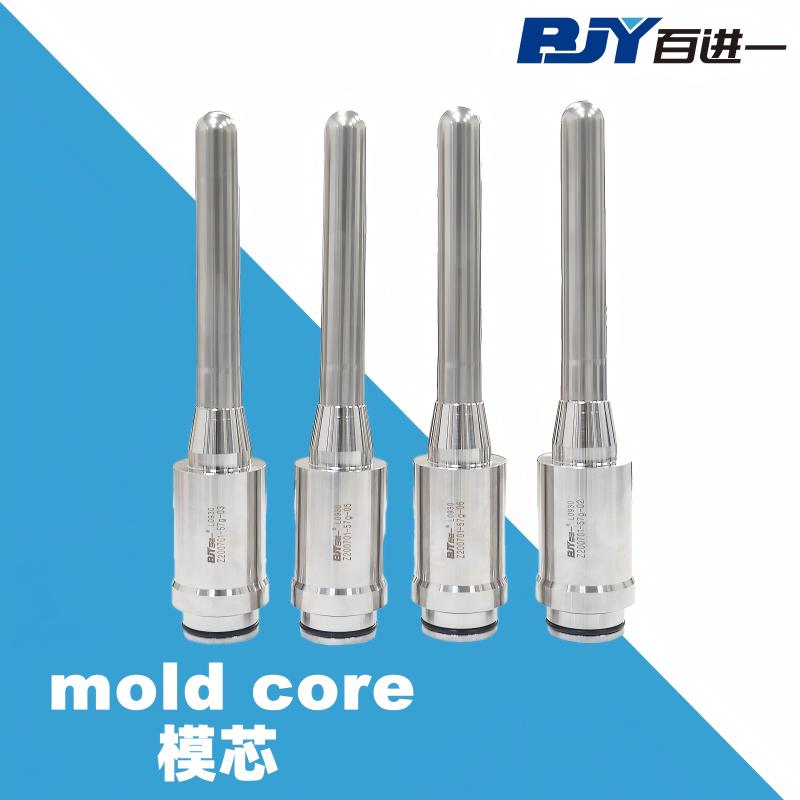
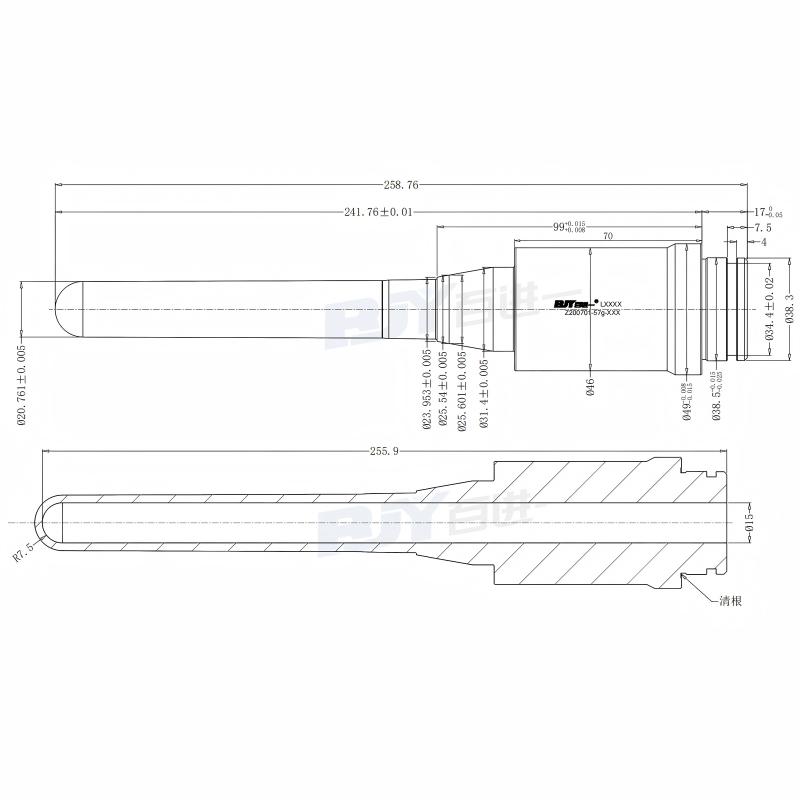
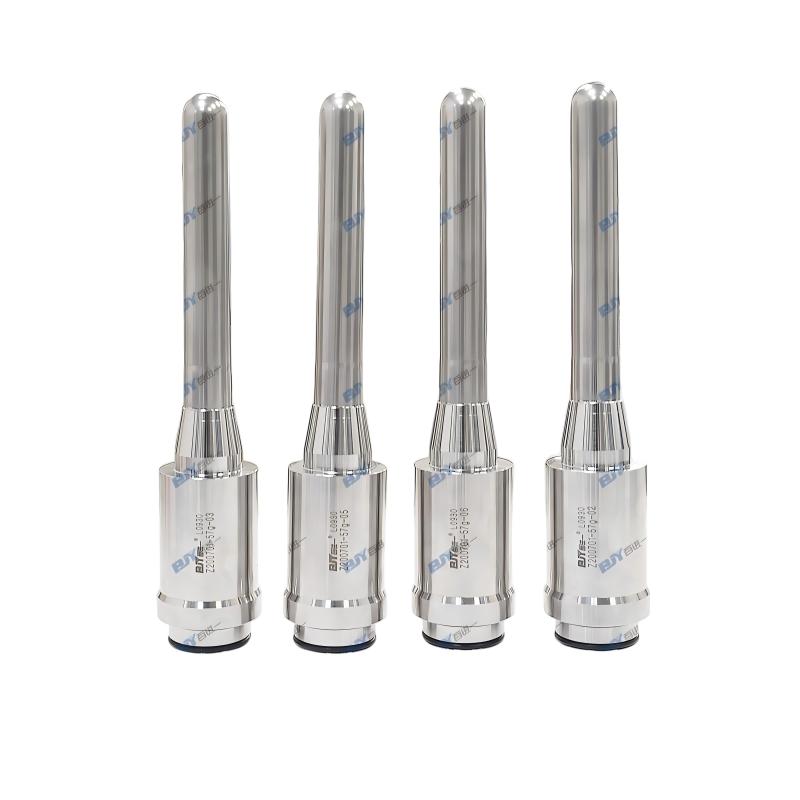
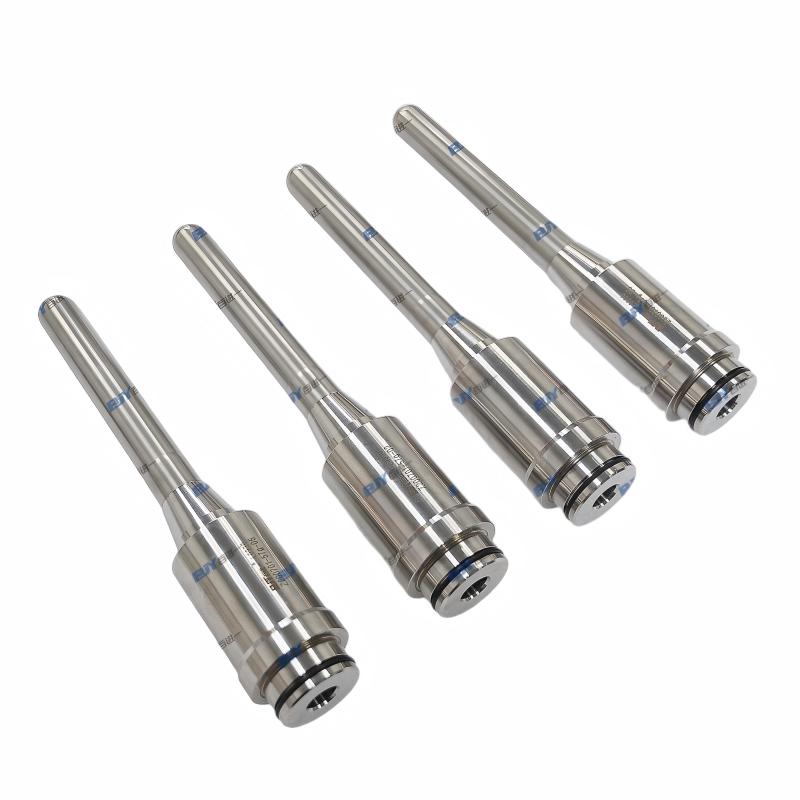
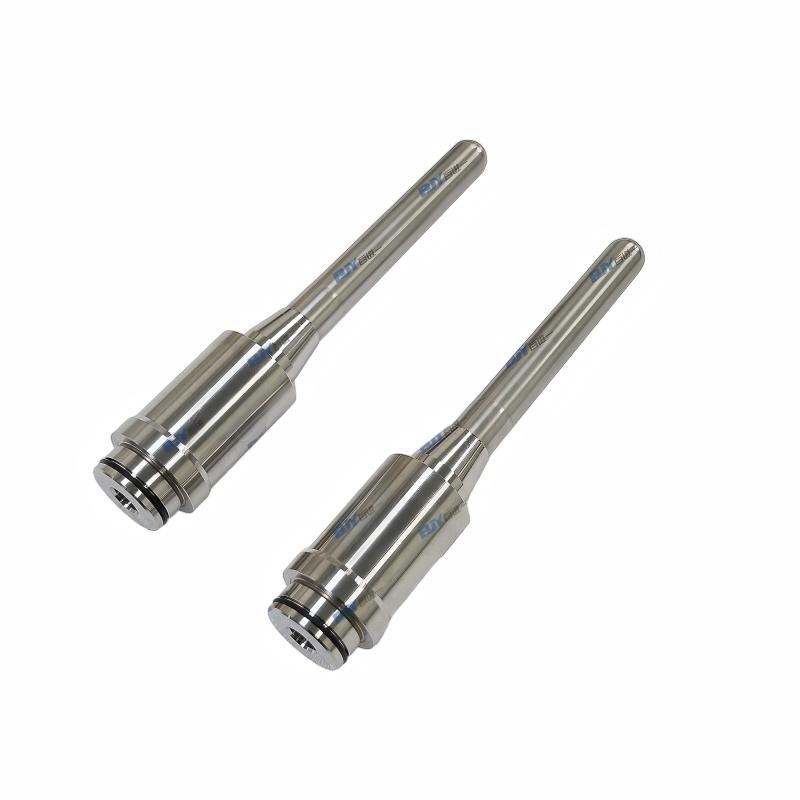
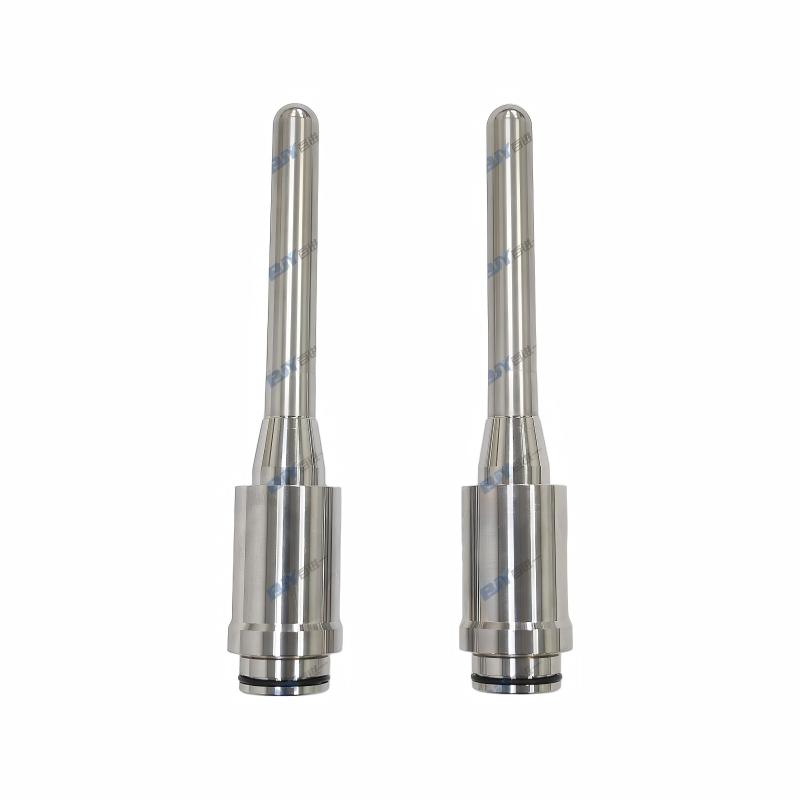
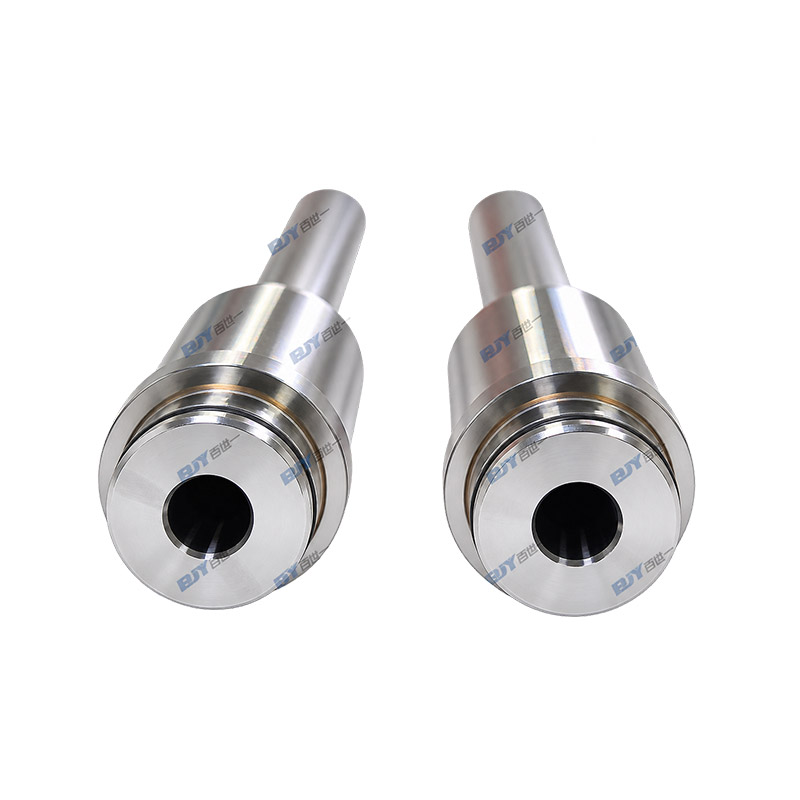
Melt goes in hot and leaves the machine as a firm tube. In between, the inside of a PET preform is being shaped by one part: the mold core. This one measures 49 × 258.76 mm and weighs 57 g. It is the inner forming member of a PET preform injection mold, made as a matched part for the tool it belongs to.
Two surfaces, one wall of plastic
Melt fills the gap between two steel surfaces. The cavity forms the outside of the preform. The core forms the bore and the inner face of the neck. Once the shot lands, neither of them works alone: same wall of plastic, same cycle, same heat to deal with.
Where the core decides the cycle
Heat is most of the story. The outside of the preform has an easy way out, straight through the cavity block, and there is plenty of metal out there to carry it away. The inside has no such road. Everything it loses has to pass through the core. Mismatch the two sides and the wall sets unevenly — thin in one place, thicker in another. You won't see it at the machine. It turns up later, when wall thickness is measured across the cavities.
Getting the preform off
Then there is release. PET shrinks as it cools, and it grips whatever is sitting inside it. Ejection is a shrinking part sliding off a polished steel rod. How much force that takes, and whether the inner wall comes away clean or marked, is settled by the finish of the forming surface. Ours is mirror level.
Small part, long campaign
A core is a modest piece of a large tool, but it repeats its work every cycle for years, and it has to behave the same way in the first cavity as in the last one. That repeatability is really what a plant buys when it buys a core.
•Forms the bore and the inner face of the neck
•Internal cooling arranged to match the cavity side
•Mirror-finished forming surface
×

Contact Us

captcha